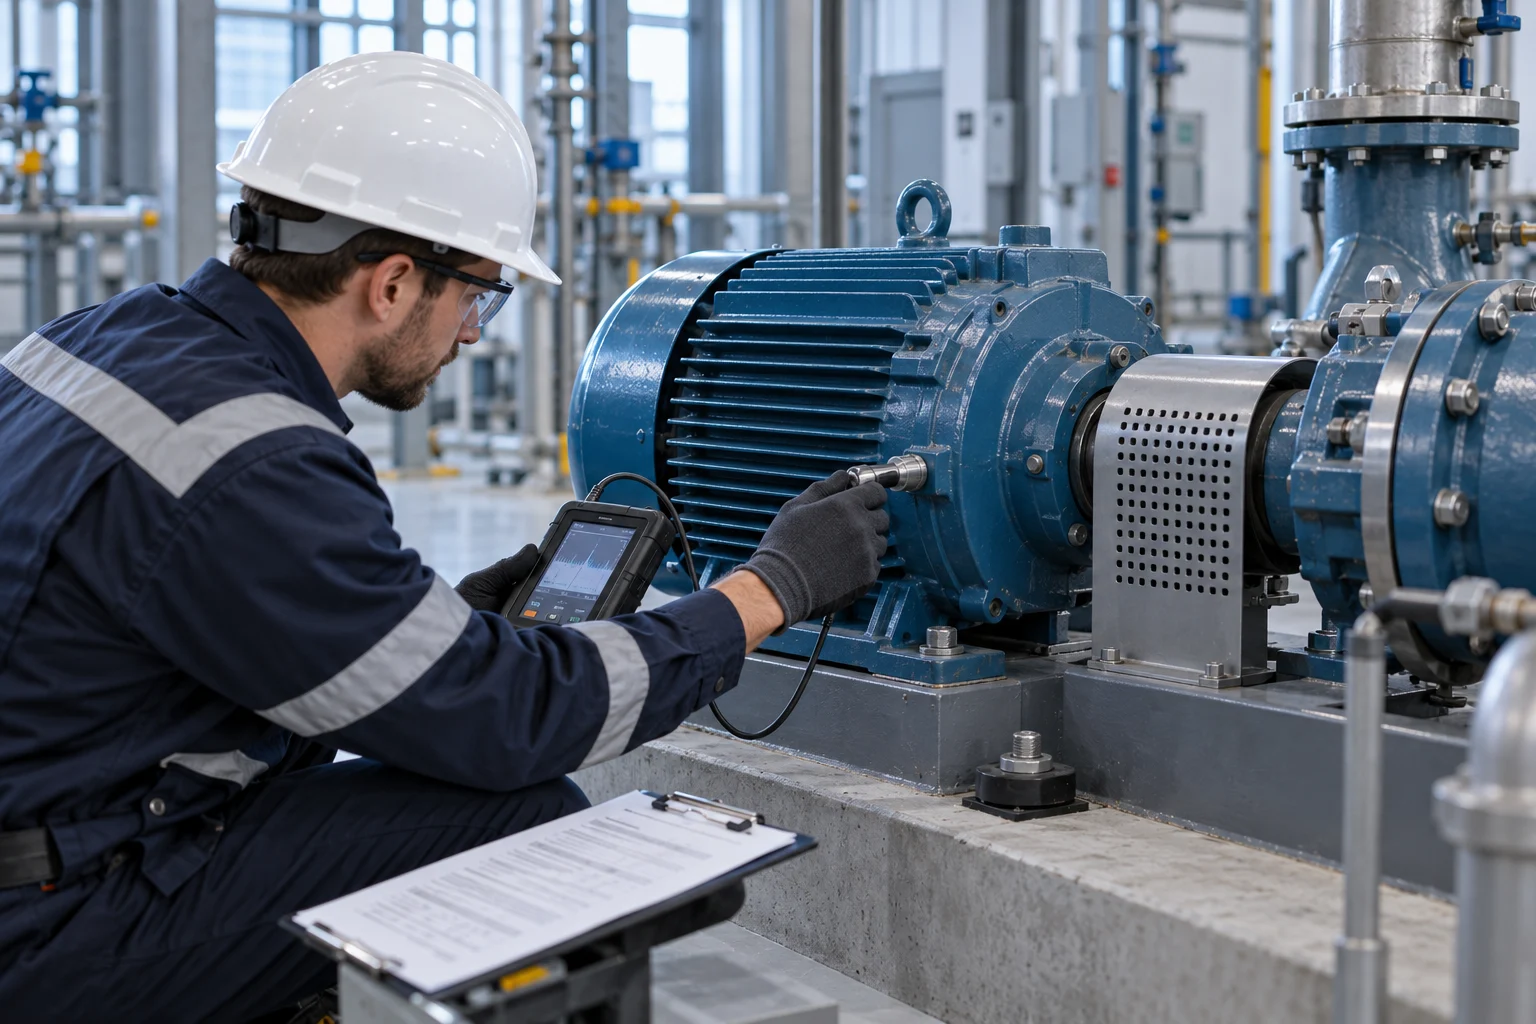
A preventive maintenance plan is not a calendar assigning every device an inspection on the same day. Assess how each failure affects production or safety, whether deterioration can be detected in advance and the risks introduced by the maintenance work itself. A good plan makes prevented losses and equipment condition visible, rather than merely counting completed tasks.
01Combine the equipment inventory with criticality assessment
The first step is an inventory of machines and their subsystems. Motors, drives, power supplies, fans, sensors and mechanical transmissions may have different maintenance requirements. Assess the production loss, quality impact, safety consequences and spare-part availability associated with each failure.
Two motors of the same model may have different maintenance priorities. One may drive a redundant auxiliary pump, while the other drives the only conveying axis for an entire line. Without this distinction, easily inspected, low-criticality equipment can fill the plan while the real bottleneck is neglected.
02Select the maintenance strategy for the failure mode
Time-based replacement, condition-based maintenance and corrective intervention after failure are different strategies. Do not assume that every component deteriorates in the same way as it ages. Regular visual checks may be sufficient for some equipment, while temperature, vibration or electrical trends may be more meaningful for others.
| Equipment / failure mode | An appropriate data example | The question the plan must answer |
|---|---|---|
| Fan and filter | Airflow, contamination, panel temperature | Under what conditions should it be cleaned or replaced? |
| Motor bearing | Vibration trend under appropriate operating conditions | Which trend will determine replacement? |
| Electrical connection | Visual / thermal inspection using an appropriate procedure | How will loosening or overheating be verified? |
| Control system | Spare-part and restoration testing | How quickly can operation be restored after failure? |
03Take measurements under comparable conditions
A motor's temperature can naturally change with load and ambient conditions. When establishing a trend, record the load, speed, environment and measurement point as well as the date. Without a baseline, a single number may be insufficient to conclude that the equipment is deteriorating.
Vibration monitoring is performed while the equipment is in a suitable operating state and using a safe measurement method. A recording taken from a stopped motor is not an operating vibration trend. Electrical insulation measurements require different preparation: connected electronics and the manufacturer's test conditions must be considered. A “one instrument for every measurement everywhere” approach is inappropriate.
04Work orders must be actionable
Instead of writing “check the panel”, specify which point must be assessed and by which method. Define the required energy isolation, permits, equipment and acceptance criteria. The work order should include a field for the measured value, the action required if a non-conformity is found and the responsible party.
Habits such as indiscriminately tightening every connection at each service can cause damage rather than help. Follow the connection type, manufacturer's torque specifications and inspection method. Maintenance aims to manage a defined failure mechanism, not unnecessarily dismantle working components.
05How should a pilot maintenance plan be evaluated?
As an example, suppose a conveyor group experiences recurring stoppages several times a month. First separate the causes: sensor contamination, mechanical jamming and drive faults should not be grouped under one heading. Prepare a work order targeting the most frequent and consequential cause. In the next period, monitor not just whether maintenance was completed but also the duration and recurrence of the relevant stoppage.
If results do not improve, review the underlying hypothesis before shortening the interval. The inspection may target the wrong point, or the problem may be inherent in the design. Adding more tasks to the maintenance checklist can increase workload without solving the underlying issue.
06Include spare parts and software in the maintenance plan
A spare drive may be on the shelf without having its parameters prepared. A PLC project may have been saved without recording the software version needed to open it. Plan stock levels, compatibility, storage and restoration conditions together for critical parts. Follow the manufacturer's maintenance guidance for items such as batteries, fans and storage media.
07The plan should be a living record
Record the completed work, measurements, defects found and corrective actions. Initiate a root-cause assessment for recurring faults. Indicators such as time between failures and repair time are useful when data definitions are consistent. The best maintenance plan is not the thickest file: it is one that is updated according to equipment condition and actually reduces production losses.
08Example verification scenario
Suppose a control-panel fan is serviced every month, yet high-temperature shutdowns continue. Check whether the filter was actually replaced, whether the airflow path is obstructed and whether the measurement point represents the hot area. A rotating fan does not prove that adequate airflow is available. The work order can be updated to record the measured temperature and observed airflow conditions rather than simply “fan checked”. Evaluate the effectiveness of the plan by comparing these records with the subsequent downtime trend.
Technical references and further reading
For product- and version-specific values, the relevant manufacturer's current documentation should be taken as the reference. The calculations and scenarios above are engineering examples for illustrative purposes.